We use cookies to help us deliver and improve this site. By clicking Confirm or by continuing to use the site, you agree to our use of cookies. For more information see our Cookie Policy.
Rotary Lobe Pumps - Michael Smith Engineers
Michael Smith Engineers supplies specialist rotary lobe pumps for hygienic and industrial applications, helping customers transfer products reliably while maintaining product quality and process efficiency. Our range includes pumps from Ampco Pumps, GEA Hilge and Viking Pump Hygienic, covering applications in food and beverage, dairy, pharmaceutical, personal care and selected chemical industries.

How do rotary lobe pumps work?
Rotary lobe pumps are positive displacement pumps. Two synchronised, non-contacting rotors turn within a pump chamber, drawing liquid through the inlet and carrying it around the casing to the outlet. This design provides controlled flow and gentle product handling, making rotary lobe pumps particularly suitable for viscous liquids, shear-sensitive products, pastes and fluids containing suspended solids.
Flow can be varied by adjusting pump speed, while a choice of rotor profiles, materials, seals and connections allows the pump to be tailored to the application.
Our rotary lobe pump ranges

Ampco AL Series
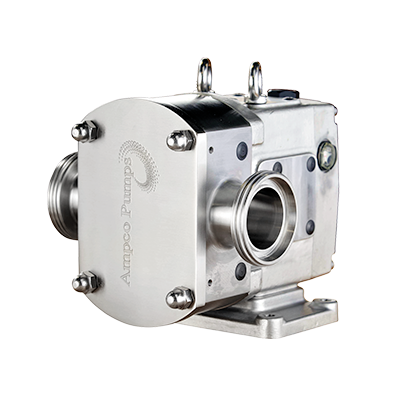
The Ampco AL Series is a versatile rotary lobe pump designed for food, beverage, dairy, pharmaceutical and industrial processing. Its 316L stainless steel wetted construction, front-loading seal arrangement and suitability for clean-in-place (CIP) operation make it a strong option for hygienic duties. Single-wing, bi-wing, tri-lobe and multi-lobe rotor options, together with a wide selection of seal arrangements and optional heating or cooling jackets, provide flexibility for demanding applications. Selected configurations are available with 3-A and EHEDG certification.
GEA Hilge NOVALOBE
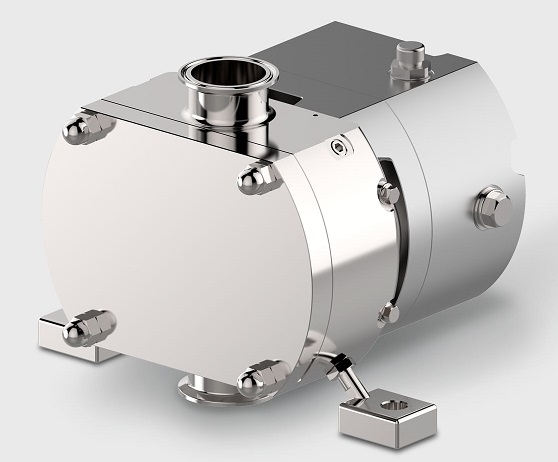
The GEA Hilge NOVALOBE range combines hygienic construction with a robust mechanical design. EHEDG-certified, it features front-loaded seals, smooth internal surfaces and a drainable design when installed in the appropriate vertical configuration. Interchangeable rotor profiles allow the pump to be adapted to different products: uni-wing rotors for gentle handling of larger solids and dough-like products, bi-wing rotors for general applications, and multilobe rotors for reduced shear and pulsation. The range is designed for differential pressures up to 16 bar.
Viking Pump Hygienic
Viking Pump Hygienic offers established rotary lobe pump solutions for food and beverage processing, dairy, pharmaceutical and personal care applications. The Classic+ / MultiPump range combines reliable pumping performance with practical maintenance and cleaning features, while the SteriLobe range is designed for demanding hygienic duties where product integrity and cleanability are priorities. These ranges offer a choice of pump sizes, rotor configurations and sealing arrangements to suit different process requirements.
Typical applications
Rotary lobe pumps are widely used for transferring chocolate, cream, yoghurt, cheese products, sauces, syrups, confectionery, cosmetics, lotions, pharmaceutical preparations and other viscous or shear-sensitive liquids. Their ability to handle suspended solids gently also makes them suitable for products where texture and appearance must be preserved.
Why choose Michael Smith Engineers?
With access to three specialist manufacturers, Michael Smith Engineers can help customers compare different rotary lobe pump designs and identify the most appropriate solution for their application. Our technical team considers product characteristics, flow rate, differential pressure, temperature, cleaning requirements and materials compatibility when recommending a pump.
From initial pump selection to spare parts, servicing and ongoing technical support, we help customers achieve dependable performance throughout the life of their equipment.
Explore our ranges:
| Pumps | Flow Range | Maximum Pressure | |
|---|---|---|---|
| Ampco AL Series | up to 100 m³/hr | 20 bar | More Info |
| GEA Hilge NOVALOBE | up to 100 m³/hr | 16 bar | More Info |
| Viking Pump Hygienic | up to 189 m³/hr | 15 bar | More Info |
Performance limits, hygienic certifications and available configurations vary by manufacturer and model. Please contact Michael Smith Engineers for application-specific selection and technical advice.